Real-time testing and simulation for battery energy storage systems
Simulation
11 / 26 / 2025

Key Takeaways
- A BMS test plan earns its value when every requirement traces to a test case and a logged result before real cells are connected.
- Test phases should run from measurement accuracy through to fault injection, with numeric entry and exit criteria gating each step.
- An emulated pack moves hazardous fault cases ahead of integration, where a failed test costs a rerun instead of hardware.
A BMS test plan structured as gated phases will send your controller to pack integration with its faults already found.
Pack integration is the most expensive place to learn that a contactor sequence is wrong. Live cells limit what you can safely provoke, and every retest costs bench time. United States generators added 10.4 GW of battery storage in 2024, and every one of those systems carries a BMS that had to prove itself first. A plan that front-loads fault testing against an emulated pack protects both the schedule and the hardware.
Strong plans share one trait. They treat BMS testing as an ordered argument, where each phase earns the right to run the next one. You’ll write requirements first, map each one to a test case, then set the criteria that open and close every phase. Hardware-in-the-loop benches make that order practical, because a simulated pack will hold any cell voltage, temperature, or fault you ask for.
What a BMS test plan needs to contain before integration
A BMS test plan needs 5 things before integration starts. It needs a requirements list, a test case for every requirement, a defined bench setup, entry and exit criteria for each phase, and a record format for results. If any one is missing, your team will end up debating readiness instead of measuring it.
Consider a 96-cell series pack for a passenger vehicle. The requirements list will include items such as opening the main contactors when any cell exceeds its overvoltage limit. The matching test case names the stimulus, the expected reaction, the time allowed, and the pass threshold. Written that way, a single line traces from a safety goal to a logged result.
Traceability is the part that teams skip under schedule pressure. It’s also the part auditors and integration leads ask for first. A plan without it produces data that can’t prove coverage. Build the trace matrix before the first test runs, because retrofitting it means repeating work.
Which BMS testing standards shape the plan’s requirements
BMS testing standards set the minimum behaviours your plan must prove, and the application decides which ones apply. Road vehicle programs work to ISO 26262 for functional safety and often UL 2580 for the battery. Stationary storage programs look to IEC 62619 and UL 1973. Shipping any lithium pack requires UN 38.3 transport testing.
A storage integrator building a containerized system shows how this plays out. The team reads IEC 62619 and pulls out each clause that touches the BMS, such as overcharge voltage control and overtemperature response. Each clause becomes a numbered requirement with its own test case. Standards rarely tell you how to build the bench or how many operating points to cover, so your plan has to add that detail. Customer specifications and your own hazard analysis will add requirements above that floor, and the plan should tag where each one came from.
How to sequence BMS test cases from signals to faults
Sequence BMS test cases from the simplest observable behaviour to the most hazardous one. Start with measurement accuracy and communication, move to state estimation and balancing, then contactor control, and finish with fault injection and protection timing. Each phase depends on the one before it, so an early failure stops the run before it wastes bench hours.
“A fault injection result means little if the voltage measurement feeding it is off by 20 mV.”
Suppose the overvoltage limit is 4.25 V and the sense channel reads low. The BMS will pass a trip test on paper and still let a cell overcharge on a pack. Measurement checks come first for that reason.
The order also shortens debugging. When a contactor test fails, you already know the inputs were good.
| Test phase | What the phase proves | What should halt the phase |
| Measurement and communication | The BMS reads cell voltage, current, and temperature within tolerance. | Any channel outside tolerance, since later results inherit the error. |
| State estimation | State of charge tracks a known reference through full charge and discharge profiles. | Estimation error that grows across cycles or temperature steps. |
| Cell balancing | Balancing starts, stops, and converges at the thresholds the design specifies. | Balancing that runs during a condition where it should stay off. |
| Contactor and precharge control | Power-up, power-down, and precharge follow the specified order and timing. | Contactors closing before precharge completes. |
| Fault injection and protection | Each protection reacts correctly and inside its allowed time for single and combined faults. | A missed or late reaction on any safety requirement. |
Keep fault tests last but never optional. They’re the cases you can’t run safely on real cells, such as a shorted sense wire, a welded contactor, or a sensor that drifts mid-charge. Plan for combinations too, since 2 mild conditions arriving at once often expose logic that a single fault never reaches.
Gate criteria that decide when each BMS test phase closes
Entry criteria state what must be true before a phase starts, and exit criteria state what must be measured before it closes. Both need numbers. A phase that opens on a frozen software build and closes on a defined pass rate gives you a decision you can defend at a readiness review.
Exit criteria for the final phase before integration on a typical program will read like the following list.
- Every safety requirement has at least one passing test case logged against it.
- Protection reactions complete inside the fault tolerant time defined in the safety concept.
- State of charge error stays within the agreed band across the temperature range.
- No open defect remains above the severity the program allows.
- The software build under test matches the build going to the pack.
The last item catches more teams than you’d expect. A late calibration change after the fault campaign means the evidence no longer describes the software on the pack. Lock the build or rerun the affected cases. Entry criteria deserve the same rigour, since calibrated sense channels and a signed-off test list keep an unready BMS off the bench.
Why an emulated pack belongs in the pre-integration plan
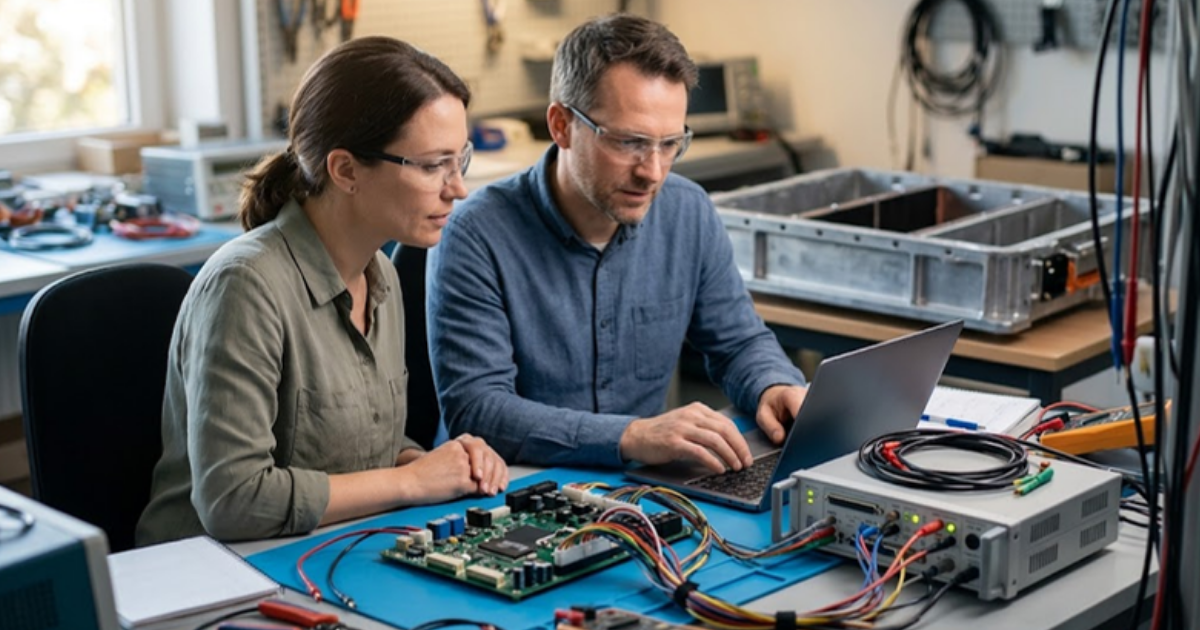
An emulated pack lets you run every case in the plan, including the destructive ones, without putting cells at risk. A real-time simulator runs the battery model and presents cell voltages, temperatures, and currents to the BMS through its normal connectors. The controller responds as it would on a pack, and you set every value.
Timing is the reason this belongs before integration. Requirements errors caught at integration and test cost 21 to 78 times more to fix than those caught while requirements are written, based on NASA’s analysis of project cost data. A bench that exercises the BMS against its requirements early moves the discovery to a place where it costs a rerun instead of a pack.
Sizing matters too. A plan for a single pack doesn’t need a rack-scale lab. OPAL-RT runs RT-LAB battery models on OP4610XG class hardware, which keeps the setup to a bench sized for one pack.
The tradeoff is model fidelity. An emulated cell behaves only as well as its parameters, so the plan should name which results need confirmation on real cells later. Thermal propagation and ageing usually sit on that list.
Common BMS test plan mistakes that surface at integration
The most common mistake is a plan that tests what the BMS does and skips what it must refuse to do. Nominal charge and discharge cases pass quickly and look like progress. Integration then exposes the untested paths, such as a wake-up during a fault or a precharge that times out.
One pattern repeats across programs. A team validates cell balancing thoroughly, then finds on the pack that the BMS closes contactors while an isolation fault is present, because nobody wrote that case. Other frequent gaps include testing only at room temperature and ignoring communication loss with the charger or vehicle controller. Each gap is cheap to close on paper. Review the plan against your hazard analysis line by line before any bench time is booked.
A disciplined plan makes pack integration a confirmation step
A well-structured BMS test plan turns pack integration into a confirmation of results you already hold. Requirements trace to cases, cases run in a deliberate order, and gates close on numbers. When the pack finally arrives, your team checks wiring and real cell behaviour instead of discovering protection logic.
That outcome comes from habits more than tools. Teams that write the exit criteria before the first test tend to argue less and ship sooner, because readiness stops being an opinion. The plan won’t remove every surprise, but it will make each one smaller and easier to explain.
“A well-structured BMS test plan turns pack integration into a confirmation of results you already hold.”
We see this at OPAL-RT when engineers bring a BMS to an emulated pack with the plan already written. The bench time goes to running cases, and the pack integration that follows is quieter for it.
Power Electronics
10 / 30 / 2026
Power shelf design for high density AI racks
How a power shelf feeds a high density AI rack, which PSU topologies and efficiency targets shape it, and how GPU load steps stress its controls.
Simulation
10 / 28 / 2026
How peers troubleshoot HIL setups faster in a forum
A practical look at how searchable peer threads shorten HIL debugging, covering recurring fault types, what a good question contains and the limits of forum answers.
Simulation
10 / 27 / 2026
A guide to the OPAL-RT engineering community
An orientation to the OPAL-RT community for new members, covering where to ask questions, what to read first, how shared models help, and how to contribute.